 50mm
 80mm
 100mm
 Hinged Doors
 Flooring U Channel
 Internal Trims
 Angles
 External Angles
 Internal Angles
 Channels
 Chiller Channel
 Freezer Channel
 Cold Room Wire Shelving
 Copper Tube
 Pipe Insulation
 Channel
 Cable Tray
 Fasteners
 Fixing Accessories
 Studding, Nuts, Bolts & Washers
 Support Frame & Mounting Block
 Tape
 Brass Fittings
 Refrigerant
 Cold Room Accessories
 Cable
 Cold Room Controller
 Cold Room Transformer
 Drain Pipe & Fittings
 Condensate Hoses
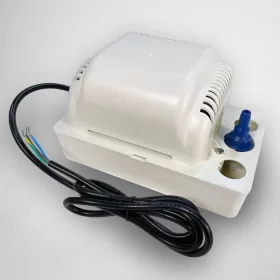 Condensate Pumps
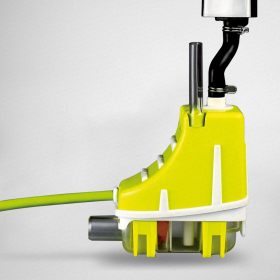 Air Conditioning Mini Pumps
 Ancillaries
 Silicon Sealant
 Expanding Foam
 Cable Ties
 Brazing
 Temperature Barrier
 Meat Hanging System
 Access Panel
 Ceiling Suspension
 Chemical
 Leak Detector
 Odour Remover
 Flooring Parts
 Checker Plate
 Tools & Workwear
Commercial Condensate Pumps for Refrigeration and HVAC Systems
Pirouz Ltd supplies a comprehensive range of commercial condensate pumps engineered for air conditioning units, commercial refrigeration displays, and walk-in cold room evaporator coils across the UK. When natural gravity drainage is unfeasible due to building layouts, high head requirements, or subterranean installations, fitting a reliable condensate pump ensures the safe and continuous removal of moisture generated during cooling cycles. We stock heavy duty tank pumps, ultra quiet mini split pumps, and robust peristaltic units designed for demanding trade environments. As a trusted UK trade supplier based in Harlow, we combine competitive pricing with fast nationwide dispatch and direct technical support for refrigeration engineers, HVAC contractors, and facility managers.
Commercial Condensate Pump Range
Selecting the correct pump mechanism depends directly on the volume of condensate produced, the available installation space, operating noise thresholds, and total discharge lift. We stock several specialized pump categories to meet exact job specifications.
Mini Split and High-Wall Condensate Pumps
Mini split condensate pumps are specifically manufactured for compact installation within wall-mounted split air conditioners, floor-standing units, ceiling cassettes, and fan coil units. These split-body systems feature a small float sensor unit placed directly inside the drain tray, connected electrically and via suction tubing to a remote pump drive module. By separating the sensor from the drive mechanism, installers can hide the main pump assembly within ceiling voids, trunking, or behind access panels, reducing audible noise in sensitive environments like offices, bedrooms, and medical consultation rooms.
Centrifugal Tank Condensate Pumps
Centrifugal tank pumps are the standard choice for heavy duty condensate management in commercial refrigeration and large capacity cooling installations. Featuring a built-in collection reservoir, durable impeller, and integrated float switch, these units automatically activate once wastewater reaches a pre-set level. Centrifugal tank pumps excel at managing high flow rates and pumping water over significant vertical distances or long horizontal pipe runs. They are widely installed beneath cold room evaporators, air handling units (AHUs), and multi-deck chiller cabinets where large volumes of water collect during defrost cycles.
Peristaltic Condensate Pumps
Peristaltic condensate pumps utilize a rotating roller mechanism against a flexible internal tube to create positive displacement suction. This design makes them exceptionally resilient in harsh or dirty operating environments where standard impellers might jam or wear prematurely. Peristaltic units are self-priming, capable of running dry without mechanical damage, and offer continuous lift even when handling water containing light dust, lint, or debris. They are frequently specified for ceiling void installations and remote drainage setups in retail and industrial buildings.
Low-Profile Under-Cabinet Refrigeration Pumps
Designed specifically for low-clearance commercial display cases in supermarkets and convenience stores, low-profile condensate pumps feature extra flat collection trays. These specialized units sit directly beneath refrigerated cabinets without requiring excavation or floor channelling. Built with oil-resistant internal components and robust motors, they process greasy or biological condensate typical of fresh food displays while preventing overflows in busy retail environments.
Technical Specifications and Performance Overview
Understanding pump performance metrics is essential to prevent water ingress, system tripping, or property damage. Below is a overview of key technical parameters available across our stocking lines:
| Pump Category | Max Flow Rate (L/h) | Max Discharge Head (m) | Operating Noise (dB(A)) | Typical Application |
|---|---|---|---|---|
| Mini Split / High-Wall | 12 to 20 L/h | 8 to 12 m | 19 to 23 dB(A) | Domestic AC, office wall splits, fan coils |
| Centrifugal Tank Pump | 180 to 500 L/h | 4 to 6 m | 40 to 48 dB(A) | Cold room evaporators, AHUs, display cabinets |
| Peristaltic Pump | 6 to 15 L/h | 12 to 15 m | 35 to 45 dB(A) | Dusty environments, ceiling voids, remote drains |
| Low-Profile Supermarket | 150 to 320 L/h | 3 to 5 m | 38 to 44 dB(A) | Under-cabinet chilled and frozen food displays |
All commercial condensate pumps supplied by Pirouz Ltd operate on standard UK 230V AC 50Hz mains power supply and incorporate high-temperature thermal overload protection. High-level safety switches come as standard on almost all commercial tank and mini pumps. These volt-free contacts (NC/NO) connect directly into the cooling equipment control circuit or building management system (BMS) to shut down refrigeration compressors or activate audible alarms before a reservoir overflows.
Integrating Condensate Management into Efficient HVAC Design
Effective condensate drainage is essential for maintaining system COP (Coefficient of Performance) and preventing premature component failure. Poor drainage causes standing water in collection trays, leading to coil corrosion, mold formation, bacterial growth, and unexpected system shutdowns. Modern high-efficiency refrigeration and air conditioning systems produce significant moisture volumes during peak thermal exchanges.
When selecting condensate pumps for modern low-carbon installations, matching pump flow rates against anticipated latent cooling loads ensures uninterrupted operation. Understanding energy efficient building services and climate controls is vital for modern building projects. You can explore more on this topic in our industry overview on HVAC’s Pivotal Role in UK Net-Zero Home Design, which highlights how precise component selection contributes to sustainable cooling and long-term energy performance across UK properties.
Selecting the Right Condensate Pump for Your Application
To choose the correct pump, contractors and engineers must consider three main variables:
- Latent Heat & Condensate Volume: Calculate the maximum potential water output based on cooling capacity (kW) and local humidity conditions. As a rule of thumb, comfort air conditioning produces approximately 0.5 to 0.8 litres of condensate per hour per kW of cooling capacity under standard conditions.
- Total Dynamic Head (TDH): Calculate the combined vertical lift requirement plus horizontal pipe friction loss. Vertical lift requires significantly more pump pressure than horizontal runs. Ensure the selected pump’s flow curve supplies sufficient output at your specific total head.
- Environmental Factors: Assess ambient noise requirements (for example, ultra-quiet operation for hotel rooms versus higher capacity industrial tank pumps for warehouse cold stores) and accessibility for routine filter cleaning and routine maintenance.
Trade Pricing, Stock Availability, and UK Delivery
Pirouz Ltd is committed to supporting refrigeration technicians, trade installers, and facility managers with reliable stock and transparent trade pricing. We maintain dedicated inventory levels at our central distribution facility in Harlow, Essex.
- Trade Pricing: Competitive trade discounts available for registered engineers, wholesalers, and volume buyers.
- Same-Day Dispatch: Orders placed before cut-off time are processed and dispatched on the same working day.
- UK Nationwide Shipping: Reliable courier shipping options including express next-day delivery across mainland UK.
- Trade Hub Pickup: Trade counter collection available directly from Unit 10, Harlow Mill Business Centre, Harlow, CM20 2FD.
Why Source Condensate Pumps from Pirouz Ltd?
Pirouz Ltd is a specialized UK trade supplier of cold room panels, doors, and commercial refrigeration components. When you partner with us for your condensate management needs, you gain access to genuine commercial quality stock, expert technical guidance, and dependable post-sale support.
Our technical team understands the field challenges faced by engineers during installation and service calls. Whether you require guidance on high-head lift calculations, safety alarm wiring, or chemical compatibility for specialized industrial drainage, we are here to provide straight technical answers and fast order fulfillment.
Frequently Asked Questions
How do I calculate the correct condensate pump size for my cooling system?
To calculate the required flow rate, multiply the total cooling capacity of your unit in kilowatts by 0.5 to 0.8 litres per hour to estimate moisture output under standard humidity. Next, measure the vertical distance from the pump location to the final discharge point, adding 1 metre of head allowance for every 10 metres of horizontal pipe run. Choose a pump whose performance curve delivers your required flow rate at that calculated total head.
Why is my condensate pump running constantly or making excessive noise?
Continuous running usually indicates a stuck float switch, a blocked check valve, airlocking in the discharge line, or a pump that lacks adequate capacity for the water volume being produced. Excessive noise can stem from dry running, worn motor bearings, vibration transferred directly to solid building structures, or debris trapped inside the impeller chamber. Regular cleaning of the reservoir and strainer screen prevents these issues.
What is the purpose of the high-level safety switch on a condensate pump?
The high-level safety switch is an independent internal float contact designed to prevent water damage if the pump fails or power is cut. By connecting these volt-free contacts (normally closed or normally open) to the refrigeration unit’s safety circuit or BMS alarm, the switch automatically shuts off the cooling equipment or triggers a visual alarm before the collection reservoir overflows.
How often should commercial condensate pumps be serviced?
In standard commercial AC applications, condensate pumps should be inspected and cleaned twice annually, usually during spring and autumn maintenance visits. In commercial food refrigeration, bakeries, or dusty manufacturing environments, quarterly inspection is recommended to clean out biological sludge, flour dust, or mineral scale build-up inside the reservoir tray and float mechanism.
Request a Quote or Order Online Today
Ready to purchase commercial condensate pumps or require technical assistance for an upcoming refrigeration project? Contact our sales team today for direct trade quotes, volume pricing, and immediate stock availability.
Pirouz Ltd
Unit 10, Harlow Mill Business Centre, Harlow, CM20 2FD
Phone: 02037508888
Website: https://www.pirouz.co.uk